
In the demanding world of hydraulic and mechanical engineering, a tube is frequently a working surface rather than simply a conduit. A hydraulic cylinder bore must seal against a piston under pressure with minimal leakage and predictable friction; a telescopic tube must slide smoothly under load; a bearing sleeve must hold its geometry through millions of cycles. Cold drawn precision seamless steel tube exists to meet those requirements, and its defining characteristic is dimensional consistency rather than pressure containment.
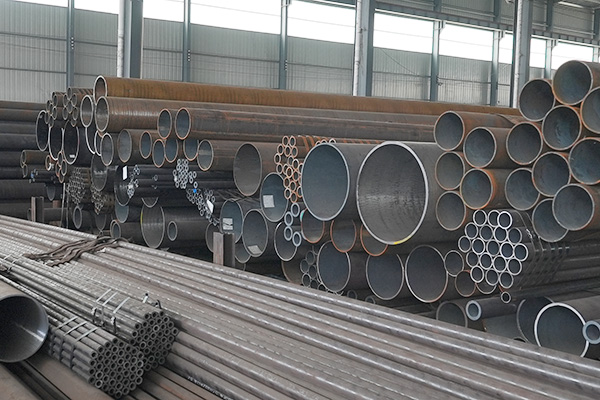
Global demand for precision tube tracks the growth of mobile hydraulics, automation equipment and lightweight automotive structures. As equipment designers raise operating pressures and reduce component size, tolerance requirements tighten accordingly.
How Cold Drawing Creates Precision
Precision tube begins as a hot finished seamless shell, which is then processed further:
Surface preparation - descaling and lubrication to prepare the shell for drawing
Cold drawing - pulling the tube through a die and over a mandrel, reducing both outside diameter and wall thickness while improving surface finish
Intermediate heat treatment - to restore ductility between drawing passes
Final heat treatment - typically normalising or stress relieving, depending on specified delivery condition
Straightening - multi-roll straightening to achieve the specified straightness tolerance
Finishing - cutting to length, end chamfering, and where specified honing or skiving of the bore
Cold working raises strength and improves surface quality, and the controlled final heat treatment determines whether the tube is supplied soft for further machining or in a higher strength condition ready for service.
Tolerance Grades and Surface Finish
Precision tube is specified by tolerance class rather than by nominal size alone. Standards such as DIN 2391 and GB/T 3639 define permitted deviation on outside diameter, inside diameter and wall thickness, plus straightness and surface roughness limits. Typical characteristics include:
Outside diameter tolerance held to a small fraction of a millimetre on standard sizes
Wall thickness concentricity controlled to support predictable machining allowance
Surface roughness maintained low enough to avoid premature seal wear
Straightness limited per metre to prevent binding in sliding assemblies
For hydraulic cylinder service the internal surface is critical. Honed or skived and burnished tube provides the bore geometry and finish that allow long seal life and low friction, typically specified by roughness value and tolerance class such as H8 or H9.
Mechanical Properties and Machinability
Cold drawn tube in the standard delivery condition offers good machinability along with improved strength relative to hot finished product. Where the application involves subsequent welding, cold forming or heavy machining, buyers should specify the delivery condition explicitly - common options include as drawn, stress relieved, annealed and normalised.
Stress relieving is particularly important where significant material will be removed during machining, because unbalanced residual stress causes distortion once the tube is cut.
Typical Applications
Hydraulic and pneumatic cylinder barrels, including telescopic cylinders
Automotive components - shock absorber bodies, steering columns, drive shafts
Machine tool spindles, guide tubes and bearing sleeves
Textile machinery rollers and printing cylinder cores
Bearing rings, bushings and precision mechanical assemblies
Pressure lines in hydraulic power units where smooth bore improves flow
Quality Control and Inspection
A capable precision tube manufacturer verifies far more than nominal size:
Dimensional inspection of outside diameter, inside diameter and wall thickness at multiple points
Concentricity and ovality measurement
Straightness verification over the full length
Surface roughness measurement, particularly for honed bore product
Surface defect inspection - visual and non-destructive testing
Mechanical testing - tensile, hardness and, where required, flattening and flaring
Cleanliness and internal surface protection for hydraulic service
Packaging matters more for precision tube than for standard pipe. Individual sleeving or wrapping, end protection and careful bundling prevent the surface damage that would otherwise render the tube unusable for machining.
Conclusion
Precision applications judge tube by geometry first and strength second. Cold drawn precision seamless steel tube delivers the dimensional tolerance, surface quality and straightness that hydraulic cylinders, machine building and automotive components depend on, with a seamless structure that supports machining, honing and welding. Working with an established China precision tube manufacturer that controls tolerance, measures surface finish and protects the product through packaging helps equipment builders hold their own assembly tolerances and reduce scrap.
Peter Nash
Mechanical Engineering Consultant, Baoyang Pipeline
Peter Nash is a mechanical engineering consultant at Cangzhou Baoyang Pipeline Equipment Co., Ltd. with fifteen years of experience in precision tube applications. He works with hydraulic cylinder manufacturers, machine builders and automotive component suppliers on dimensional tolerance, surface finish, straightness and material specification for cold drawn and honed tube.